Which ISO Certification Is Best for Manufacturing Companies?
Which ISO Certification Is Best for Manufacturing Companies?
Introduction
Manufacturing companies must maintain consistent product quality, control production costs, follow safety regulations, and meet customer expectations. Whether you manufacture automobile parts, electrical equipment, packaging materials, machinery, chemicals, or industrial products, having a well-managed production system is essential for long-term business growth.
This is where ISO certification for manufacturing companies becomes valuable.
ISO certification helps manufacturers establish systematic processes, improve product quality, reduce operational risks, and build trust among customers. It can also strengthen your company's position when participating in government tenders, supplying products to large organizations, or entering international markets.
But which ISO certification is best for manufacturing companies?
The answer depends on your industry, production activities, customer requirements, environmental responsibilities, and workplace safety risks.
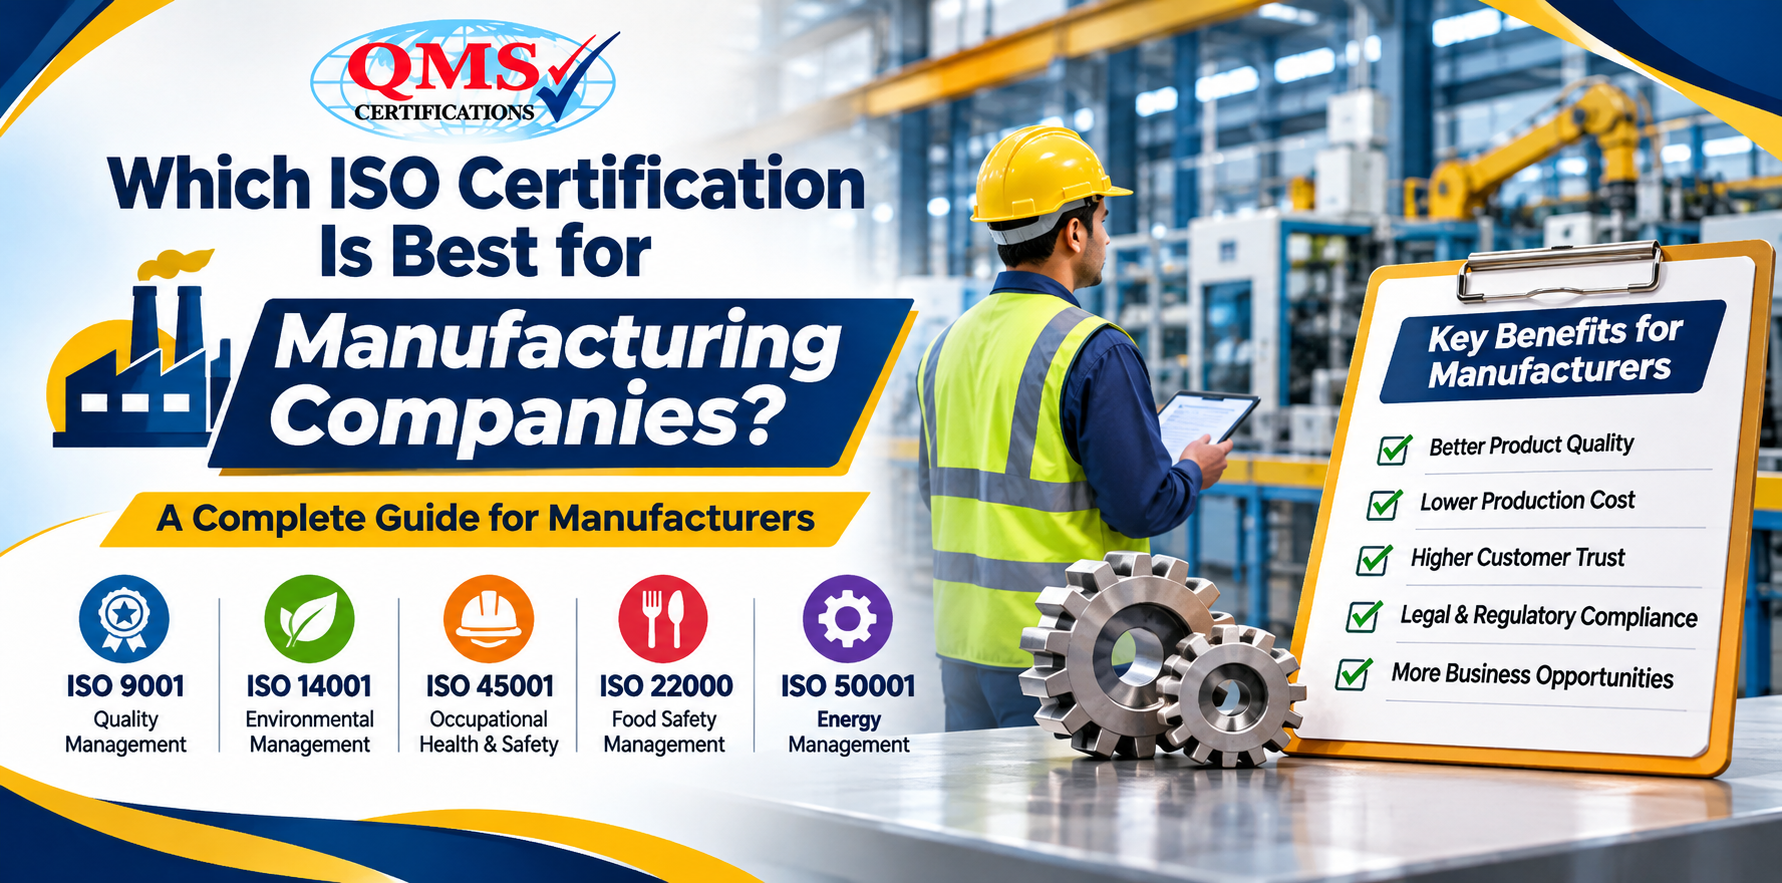
For most manufacturing businesses, ISO 9001 is the recommended starting point, while ISO 14001 and ISO 45001 provide additional benefits in environmental management and occupational health and safety.
Let's understand the most suitable ISO certifications for different manufacturing businesses in India.
Which ISO Certification Is Best for Manufacturing Companies?
The following ISO standards are particularly relevant to manufacturing industries:
|
ISO Standard |
Main Purpose |
Suitable For |
|---|---|---|
|
ISO 9001 |
Quality Management |
All manufacturing companies |
|
ISO 14001 |
Environmental Management |
Factories and industrial units |
|
ISO 45001 |
Occupational Health & Safety |
Factories with workplace risks |
|
ISO 22000 |
Food Safety Management |
Food and beverage manufacturers |
|
ISO 13485 |
Medical Device Quality Management |
Medical equipment manufacturers |
|
ISO 50001 |
Energy Management |
Energy-intensive manufacturing units |
1. ISO 9001 – Quality Management System
Best starting point for manufacturers
ISO 9001 is one of the most widely recognized quality management standards worldwide. It helps manufacturing companies establish consistent production processes and deliver products that meet customer and applicable regulatory requirements.
For example, an automobile component manufacturer in India may receive complaints about inconsistent product dimensions. By implementing ISO 9001, the company can introduce standardized inspection procedures, maintain production records, train employees, and monitor product quality.
Key benefits of ISO 9001:
-
Improves product quality and consistency.
-
Reduces manufacturing defects and rework.
-
Improves customer satisfaction.
-
Establishes systematic production procedures.
-
Supports supplier evaluation and quality control.
-
Strengthens business credibility and tender eligibility.
ISO 9001 is suitable for small manufacturing units, medium-sized factories, large industrial companies, and export-oriented businesses.
Important update: ISO 9001:2026 was published on 16 September 2026. Companies planning new certification or transitioning from an earlier version should confirm the applicable certification and transition arrangements with their certification body.
Quality management systems — Requirements+1
2. ISO 14001 – Environmental Management System
Manufacturing activities can generate industrial waste, air emissions, wastewater, and high energy consumption. ISO 14001 helps companies identify and manage their environmental impacts.
For example, a plastic manufacturing company can use an environmental management system to monitor waste disposal, reduce material wastage, improve resource utilization, and manage pollution-related responsibilities.
Key benefits of ISO 14001:
-
Improves environmental performance.
-
Supports pollution prevention.
-
Helps manage industrial waste.
-
Encourages efficient resource utilization.
-
Supports compliance with applicable environmental requirements.
-
Builds a responsible business reputation.
It is particularly useful for chemical factories, plastic manufacturers, textile industries, engineering units, and other businesses with significant environmental impacts.
3. ISO 45001 – Occupational Health and Safety Management
Factory workers regularly operate machinery, handle industrial equipment, and work in environments where occupational hazards may exist.
ISO 45001 provides a structured approach to identifying workplace hazards, assessing safety risks, preventing accidents, and improving employee safety.
For example, a metal fabrication company can introduce machine safety procedures, personal protective equipment requirements, employee safety training, and emergency response arrangements.
Key benefits of ISO 45001:
-
Reduces workplace accidents and injuries.
-
Improves employee safety awareness.
-
Identifies and controls occupational hazards.
-
Establishes emergency preparedness procedures.
-
Improves workplace safety management.
-
Demonstrates commitment to employee welfare.
This certification is especially valuable for engineering, automobile, construction material, chemical, and heavy manufacturing industries.
ISO
4. ISO 22000 – Food Safety Management System
Food manufacturers must maintain hygiene, control contamination risks, and ensure that food products remain safe throughout production and handling.
ISO 22000 establishes a food safety management framework that includes hazard identification, food safety controls, and systematic monitoring.
It is suitable for:
-
Food processing companies.
-
Dairy product manufacturers.
-
Packaged food manufacturers.
-
Beverage production units.
-
Food ingredient manufacturers.
5. ISO 13485 – Medical Device Quality Management
ISO 13485 is designed for organizations involved in manufacturing and supplying medical devices.
It focuses on quality management, product traceability, risk management, and applicable regulatory requirements throughout the medical device lifecycle.
It is suitable for manufacturers of surgical instruments, diagnostic equipment, medical disposables, and other medical devices.
6. ISO 50001 – Energy Management System
Manufacturing industries often consume significant electricity, fuel, and other energy resources.
ISO 50001 helps organizations monitor energy usage, identify inefficiencies, establish energy performance objectives, and improve energy management.
It is particularly relevant to steel plants, textile factories, cement manufacturers, and other energy-intensive industries.
Why Choose QMS Certificate for ISO Certification?
Selecting the right certification guidance is just as important as selecting the right ISO standard. Every manufacturing business has different production activities, documentation requirements, and operational challenges.
At QMS Certificate, we help businesses understand the certification requirements and prepare for their ISO certification journey.
Why work with us?
-
Industry-oriented guidance: Understand which ISO standard matches your manufacturing activities.
-
Documentation assistance: Get guidance on preparing quality manuals, procedures, policies, and required records.
-
Implementation support: Develop practical management system processes for your business.
-
Audit preparation: Understand internal audit requirements and prepare for certification audits.
-
Business-focused approach: Build a management system that supports your actual operations rather than unnecessary paperwork.
Our objective is to make the ISO certification process easier to understand and more manageable for manufacturing businesses.
Key Benefits of ISO Certification for Manufacturing Companies
ISO certification offers more than a certificate for display. When properly implemented, it can improve everyday factory operations.
1. Better product quality: Standardized processes help manufacturers maintain consistent product specifications.
2. Reduced production costs: Identifying defects, rework, and process inefficiencies can help reduce unnecessary expenses.
3. Improved customer confidence: Customers gain greater confidence when a manufacturer follows a recognized management system.
4. Better business opportunities: ISO certification may help meet supplier qualification requirements and support participation in eligible tenders.
5. Improved employee performance: Defined responsibilities, training, and documented procedures help employees understand their roles.
6. Stronger operational control: Regular monitoring, internal audits, and management reviews help identify problems before they become serious.
7. Better export readiness: International customers may consider ISO certification when evaluating suppliers, although certification alone does not guarantee export approval.
Step-by-Step ISO Certification Process for Manufacturing Companies
The ISO certification process generally involves the following stages:
CERTIFICATION ROADMAP
-
Step 1: Identify the correct ISO standard
Evaluate your manufacturing activities, customer expectations, industry requirements, and operational risks.
-
Step 2: Conduct a gap analysis
Review existing production procedures and identify areas that need improvement to meet the selected ISO standard.
-
Step 3: Prepare ISO documentation
Develop the necessary policies, procedures, work instructions, inspection records, and management system documents.
-
Step 4: Implement the management system
Apply the documented processes across relevant departments, including production, quality control, stores, and maintenance.
-
Step 5: Conduct employee training
Train employees on quality requirements, operational procedures, responsibilities, and applicable safety practices.
-
Step 6: Perform internal audits
Evaluate whether the management system is properly implemented and identify any nonconformities.
-
Step 7: Complete the certification audit
The selected certification body assesses the management system against the applicable ISO requirements.
-
Step 8: Receive the ISO certificate
Once the applicable requirements are fulfilled and certification is approved, the certification body issues the certificate.
The actual timeline depends on company size, operational complexity, number of employees, and management system readiness.
Documents Required for ISO Certification in Manufacturing Industry
The documents required depend on the selected ISO standard and the company's activities. However, manufacturing companies commonly need the following:
-
Company registration certificate or business registration proof.
-
PAN card and applicable business identification details.
-
Factory address and operational details.
-
Manufacturing process flowchart.
-
Organizational structure and employee responsibilities.
-
Quality policy and quality objectives (for ISO 9001).
-
Production and inspection procedures.
-
Machinery and equipment maintenance records.
-
Raw material and supplier evaluation records.
-
Employee training and competency records.
-
Product inspection and testing records.
-
Internal audit reports.
-
Management review records.
-
Corrective action and nonconformity records.
Additional documents may be required for environmental, occupational health and safety, food safety, or medical device management systems.
Note: Documentation should reflect actual business activities. Companies should not create misleading records or claim compliance with processes that have not been implemented.
Which ISO Certification Should Your Manufacturing Company Choose?
The right ISO certification depends on your manufacturing sector and business objectives.
|
Manufacturing Business |
Recommended ISO Certification |
|---|---|
|
Automobile parts manufacturing |
ISO 9001 + ISO 14001 + ISO 45001 |
|
Plastic manufacturing |
ISO 9001 + ISO 14001 |
|
Textile manufacturing |
ISO 9001 + ISO 14001 + ISO 45001 |
|
Food manufacturing |
ISO 22000 + ISO 9001 |
|
Pharmaceutical manufacturing |
ISO 9001 / applicable GMP requirements |
|
Medical equipment manufacturing |
ISO 13485 |
|
Steel and metal manufacturing |
ISO 9001 + ISO 14001 + ISO 45001 |
|
Electrical equipment manufacturing |
ISO 9001 + ISO 14001 |
|
Machinery manufacturing |
ISO 9001 + ISO 45001 |
|
Energy-intensive manufacturing |
ISO 9001 + ISO 50001 |
These are general recommendations. The final selection should consider applicable sector regulations, customer specifications, and business requirements.
Frequently Asked Questions (FAQs)
1. Which ISO certification is best for manufacturing companies?
ISO 9001 is generally the best starting point for manufacturing companies because it focuses on quality management, production consistency, customer satisfaction, and continuous improvement. Companies can also consider ISO 14001 and ISO 45001 depending on their environmental and workplace safety requirements.
2. Is ISO 9001 mandatory for manufacturing companies in India?
ISO 9001 is generally not legally mandatory for every manufacturing company in India. However, certain customers, buyers, government tenders, and supplier agreements may require ISO 9001 certification as part of their qualification criteria.
3. Can a small manufacturing company get ISO certification?
Yes. Small manufacturing companies, MSMEs, startups, and large industrial organizations can all obtain ISO certification. The management system should be designed according to the company's size, activities, products, and operational complexity.
4. What documents are required for ISO certification in manufacturing industries?
Common documents include business registration proof, PAN details, manufacturing process flowcharts, quality policies, production records, inspection reports, employee training records, equipment maintenance records, internal audit reports, and management review records.
5. How long does it take to get ISO certification for a manufacturing company?
The timeline depends on the company's size, number of employees, manufacturing processes, documentation readiness, and audit requirements. A relatively simple manufacturing unit may complete the process faster than a large factory with multiple production locations and complex operations.
Conclusion: Choose the Right ISO Certification for Long-Term Manufacturing Growth
Choosing the best ISO certification for manufacturing companies is an important decision that can influence product quality, operational efficiency, customer confidence, and business opportunities.
For most manufacturers, ISO 9001 is an excellent starting point. Businesses looking to improve environmental performance can consider ISO 14001, while companies focusing on employee safety should consider ISO 45001. Specialized industries may require standards such as ISO 22000 or ISO 13485.
The key is to select a certification that matches your actual manufacturing activities and business objectives.
Looking for ISO certification for your manufacturing company in India?
QMS Certificate can help you understand the applicable ISO standards, documentation requirements, implementation process, and certification audit preparation.
Get in touch with our team to discuss your certification requirements.
Contact QMS Certificate
-
Website: https://www.qmscertificate.com/
-
Email: info@qmscertificate.com
Start building a stronger quality management system for your manufacturing business today.
Having any Query? Talk to our Experts
Our Projects are fully tested, background checked, license validated and insured
with a 100% satisfaction guarantee.
Contact Info
 qmscertify@gmail.com
 View Location Map


